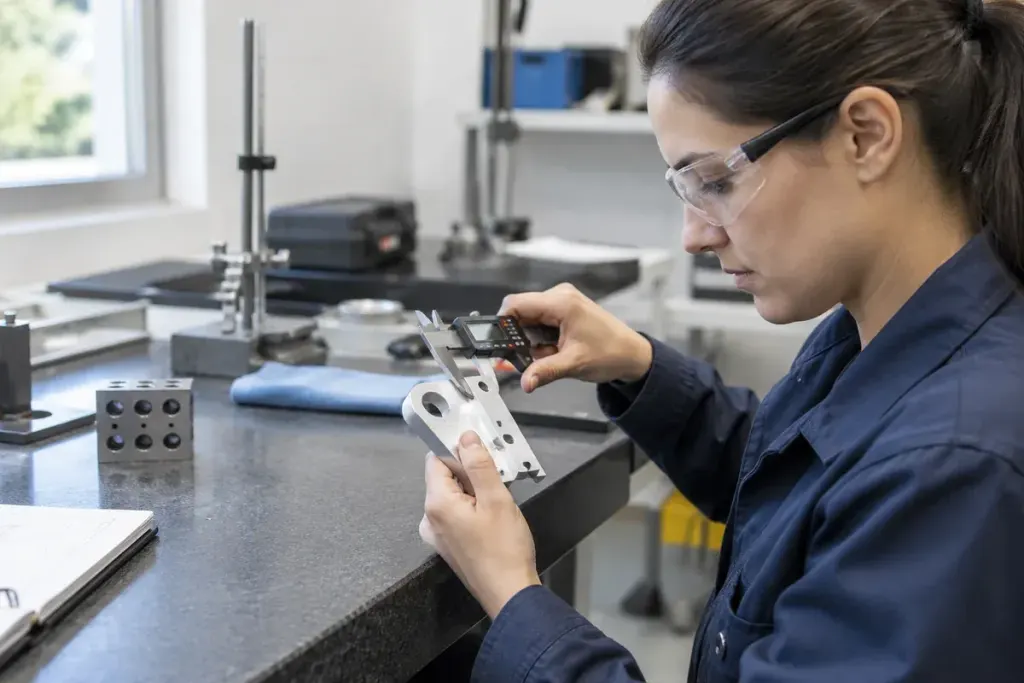
A calliper displays 20.04 mm. Is the part acceptable? The number alone cannot answer. You need to know which feature was measured, what the drawing requires and whether the measurement method is suitable for that decision.
Inspection becomes more reliable when the acceptance requirement is defined before the result appears on the screen.
Separate three different ideas
The nominal dimension is the specified reference size. The tolerance describes permitted variation under the applicable drawing or specification. Measurement uncertainty describes doubt associated with the measured value; it is not an extra allowance that can simply be added to the tolerance.
NIST’s measurement-uncertainty resources explain why a measurement result requires more context than a displayed number. The agreed inspection procedure should establish how uncertainty and acceptance decisions are handled.
Read the drawing revision and feature
Confirm the part number, revision, units and exact feature. A dimension taken across the wrong surfaces may be repeatable and still irrelevant. Check any general tolerances and feature-specific requirements rather than assuming every dimension follows the same limit.
For a simplified example, a dimension of 20.00 mm with a stated tolerance of plus or minus 0.10 mm gives nominal limits of 19.90 and 20.10 mm. Real acceptance still depends on the specified method and decision rule; the example is arithmetic, not a universal inspection procedure.
Use an appropriate method
Instrument resolution, calibration status, contact technique, part condition and temperature can matter. A digital display with several decimal places does not establish that the measurement is accurate enough for the requirement.
Follow the controlled procedure and use trained personnel. If results are close to a limit or inconsistent, escalate for the prescribed review rather than selecting the most favourable reading. Repeating a measurement without understanding the variation can hide the problem.
Make the record reconstructable
Record the part and revision, feature, instrument identifier, result, applicable limits and decision. Include the operator and date, along with environmental or preparation information required by the procedure. A bare “pass” is difficult to investigate later.
When a nonconformance appears, preserve the result and follow the organisation’s disposition process. Do not quietly widen a tolerance to match available parts. Clear requirements protect both production and the customer by making acceptance a shared rule rather than an improvised judgement at the inspection bench.